
 English
 Español
Submit feedback
Working with a China Mold Manufacturer: What Should Overseas Buyers Clarify First
Developing a custom plastic injection mold involves more than turning a product drawing into a finished tool. Overseas buyers also need to consider engineering communication, tooling specifications, production responsibilities, quality requirements, and international delivery arrangements. A clear agreement at the beginning of a project helps both parties manage technical expectations and commercial risks throughout the manufacturing process.
At Lingfei, we work with international customers on custom injection mold development and plastic component manufacturing. Our experience shows that many project difficulties can be reduced through detailed technical discussions before machining begins. Buyers working with a china plastic injection mold manufacturer should pay attention to several important areas rather than comparing quotations based on tooling prices alone.
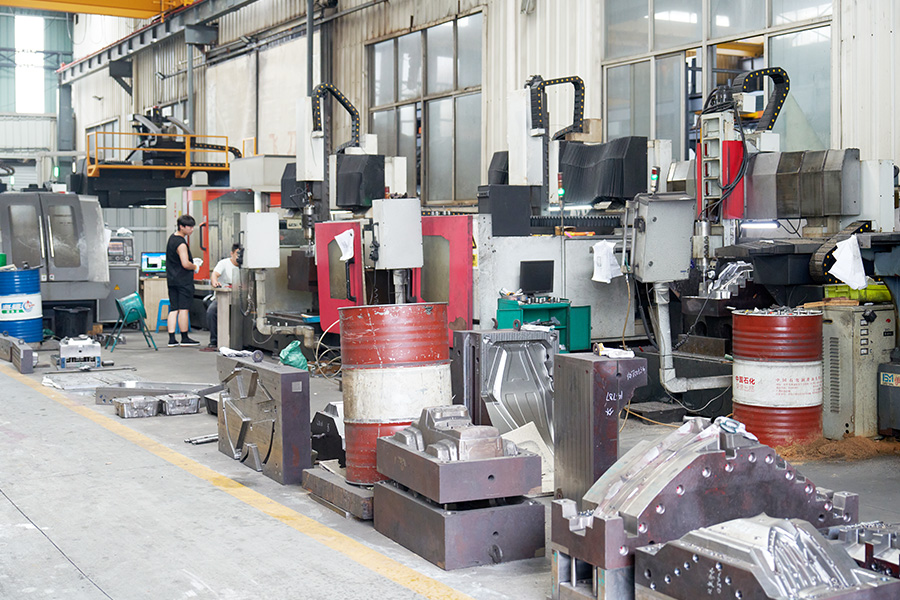
1. Define Product Requirements Before Requesting a Quotation
A mold quotation depends heavily on the geometry, material, dimensions, surface requirements, and intended production volume of the plastic component. Incomplete project information can result in inaccurate cost estimates or different technical assumptions between the buyer and manufacturer.
We recommend preparing a structured RFQ package containing the following information:
- 2D engineering drawings: Include overall dimensions, critical measurements, dimensional tolerances, and sectional views where necessary.
- 3D CAD files: STEP, IGES, or native CAD formats help our engineering team review product geometry and mold construction requirements.
- Plastic material: Specify the required resin, such as ABS, PP, PC, PA66, POM, or another engineering plastic, together with the exact grade where available.
- Surface requirements: Identify polished, textured, matte, painted, or other finishing expectations.
- Production demand: Provide estimated annual consumption and expected order patterns to support cavity configuration and tooling design decisions.
- Application details: Explain the component's function, assembly position, operating conditions, and any relevant performance requirements.
For example, an ABS electrical enclosure and a PA66 automotive connector may have similar external dimensions but require different considerations for shrinkage, material flow, wall thickness, and mold temperature. Understanding these details helps us develop a more suitable tooling proposal.
2. Review the DFM Analysis and Mold Design Proposal
Design for Manufacturing (DFM) is an important engineering step before mold production. It allows our team to identify potential manufacturing difficulties and recommend design adjustments before committing resources to mold machining.
At Lingfei, our engineering review focuses on several technical areas:
Wall Thickness and Material Flow
Uneven wall thickness can contribute to sink marks, internal stress, and dimensional deformation. A relatively uniform wall structure generally supports more predictable material flow and cooling. As a preliminary design reference, many general-purpose plastic parts use wall thicknesses around 1.5–3.5 mm, although the appropriate range depends on resin grade, component dimensions, and structural requirements.
Draft Angles and Ejection
Draft angles help molded components release from the cavity and core surfaces. General starting values may range from approximately 0.5° to 2°, while textured surfaces or deeper features can require additional draft. Our engineers evaluate the part geometry, surface finish, and ejection arrangement before confirming the design.
Gate, Runner, and Cooling Layout
Gate positioning affects filling balance, weld line location, and visible gate marks. Cooling channels also influence cycle consistency and dimensional stability. A suitable cooling arrangement should distribute heat effectively across the mold rather than concentrating cooling in only a few areas.
Buyers should request a DFM report or marked-up drawing showing proposed changes, potential risks, and unresolved engineering questions. Written approval of the revised design provides a clear reference for subsequent tooling work.
3. Confirm Mold Structure, Steel Grade, and Cavity Configuration
Different injection molding projects require different tooling structures. A simple household plastic component may use a conventional two-plate mold, while complex parts with side openings, internal threads, or undercuts may require sliders, lifters, or specialized core mechanisms.
Several mold specifications deserve particular attention during technical discussions:
- Mold base: Confirm dimensions, construction standards, and compatibility with the intended injection molding machine.
- Mold steel: Common options include P20, 718H, H13, and S136. The appropriate grade depends on production volume, resin characteristics, surface requirements, and corrosion resistance.
- Cavity quantity: Single-cavity, two-cavity, and multi-cavity configurations involve different tooling investments and production considerations.
- Runner system: Discuss cold runner or hot runner arrangements according to material consumption, part geometry, and production requirements.
- Expected mold service life: Establish the target shot count and maintenance conditions rather than relying on an unspecified durability statement.
For example, P20 steel is commonly considered for general production tooling, while S136 may be appropriate for applications requiring improved corrosion resistance or high-quality polished surfaces. These materials are not interchangeable in every application, so our recommendation should reflect the actual operating conditions.
We also encourage buyers to clarify whether the quoted tooling price includes standard accessories, spare inserts, cooling connectors, and any special mechanisms. Such details make supplier quotations easier to compare.
4. Establish Clear Mold Ownership and Intellectual Property Terms
Mold ownership is a commercial issue that deserves written confirmation before tooling payments are arranged. Overseas buyers may finance custom molds but overlook the practical details concerning storage, maintenance, technical files, and future mold transfers.
Our recommended discussion points include:
- Ownership confirmation: Specify who owns the complete mold after payment and whether ownership covers all cavities, inserts, and interchangeable components.
- CAD documentation: Define which 2D drawings, 3D files, and mold design records will be provided.
- Exclusive production: Clarify whether the mold is dedicated to the buyer's project and whether third-party production is permitted.
- Storage arrangements: Agree on the storage location, maintenance responsibilities, and conditions for long-term inactivity.
- Transfer procedures: Establish how the mold and related technical documents can be released or transferred to another facility if the business arrangement changes.
Confidentiality and intellectual property protection also deserve attention. Product drawings, CAD models, branding details, and custom engineering solutions should be handled under agreed confidentiality terms. A written agreement helps establish responsibilities for protecting project information.
5. Agree on Trial Molding and Sample Approval Criteria
Completing mold machining does not automatically mean that the tooling is ready for mass production. Trial molding allows our engineering team to evaluate mold operation, material filling, cooling performance, ejection, and molded-part dimensions.
Buyers should understand the purpose of different trial stages and the evidence required for approval.
T0 and T1 Mold Trials
A T0 trial is generally used to evaluate initial mold operation and identify potential tooling issues. Our team may review incomplete filling, flash, sink marks, weld lines, warpage, and ejection problems.
Following necessary adjustments, a T1 trial can provide additional samples for engineering evaluation. However, trial labels do not represent universal acceptance standards. Both parties should agree on the sample requirements and approval conditions in advance.
Dimensional and Appearance Inspection
Sample approval should cover measurable specifications as well as visual quality. Depending on the component, relevant inspection items may include:
- Critical dimensions and dimensional tolerances.
- Wall thickness and overall component geometry.
- Surface defects, flash, scratches, and sink marks.
- Assembly fit and functional performance.
- Material identification and color consistency.
For precision components, a coordinate measuring machine (CMM), digital calipers, micrometers, and other suitable measuring instruments can support dimensional verification. The inspection method should match the required tolerance and measurement characteristics.
We recommend establishing an inspection report format that records drawing revisions, measured values, acceptance criteria, and outstanding issues. Physical samples and inspection records should be reviewed together before production release.
6. Compare Quotations Beyond the Total Tooling Cost
Price differences between Chinese mold manufacturers do not always represent differences in manufacturing efficiency. They may reflect different mold structures, steel grades, machining processes, inspection arrangements, or included services.
At Lingfei, we encourage overseas customers to examine the quotation line by line. The following comparison areas can help clarify the actual project scope:
- Engineering charges: Check whether DFM analysis, mold design, and design revisions are included.
- Tooling specifications: Compare steel grades, mold bases, cavity counts, runner systems, and special mechanisms.
- Trial arrangements: Confirm the number of included trial rounds, sample quantities, and modification responsibilities.
- Inspection services: Identify whether dimensional reports, material documentation, and sample evaluation are covered.
- Additional costs: Clarify transportation, export packaging, spare parts, and engineering changes.
- Payment schedule: Agree on the deposit, progress payments, sample approval conditions, and final balance arrangements.
A detailed quotation creates a shared commercial reference and helps prevent unexpected charges during the project. It also allows buyers to assess the actual engineering and manufacturing services behind the proposed price.
7. Set Project Communication and Delivery Responsibilities
International mold development involves multiple communication stages, including drawing review, design approval, machining updates, mold trials, sample inspection, and shipment preparation. Differences in time zones and technical terminology can make project coordination more challenging.
We suggest establishing a practical communication arrangement before production begins:
- Assign technical contacts: Identify the engineering representative and commercial contact responsible for different project matters.
- Use revision-controlled files: Maintain consistent drawing numbers and CAD revisions to avoid manufacturing from outdated information.
- Schedule progress updates: Agree on reporting intervals and the information required at each manufacturing milestone.
- Document engineering changes: Record any changes affecting tooling design, cost, specifications, or the project schedule.
- Confirm export arrangements: Discuss protective packaging, rust prevention, loading requirements, shipping documents, and agreed Incoterms.
Delivery planning should also identify the destination port or facility, transportation responsibilities, customs documentation, and the expected shipment window. A clear division of responsibilities helps both parties coordinate international logistics more effectively.
8. Evaluate the Manufacturer's Long-Term Technical Support
Custom injection molds may require maintenance, replacement inserts, design modifications, and process adjustments during their service life. The manufacturer's support capabilities therefore matter beyond the initial tooling order.
Before establishing a long-term relationship, buyers can discuss the following service areas:
- Availability of mold maintenance and repair services.
- Technical assistance for dimensional or molding defects.
- Replacement of damaged inserts and mold components.
- Support for product redesign and engineering modifications.
- Documentation of mold maintenance and repair activities.
A capable china plastic injection mold manufacturer should be able to explain how technical problems are investigated, how corrective actions are documented, and how tooling condition is maintained. Buyers can also request relevant project examples to understand the manufacturer's experience with similar components and mold structures.
The company focuses on the field of special equipment manufacturing, and its core business revolves around the design, manufacturing and related technical services of injection molds.
© Taizhou Lingfei Mould & Plastic Technology Co., Ltd.
OEM Injection Mold Factory
